
Sampling to Inline: Multisensor Metrology in Electronics Manufacturing
The finer electronics manufacturing gets, the harder quality control becomes to sustain with manual visual inspection and offline sampling. Irregular thin-wall parts such as foldable hinges, battery housings and package substrates often need flat dimensions, step differences, warpage and surface defects measured in a single clamping; high-end lines are also replacing some sampling with inline 100% inspection. Inspection is shifting from "catching defects afterward" to "feeding back process parameters," and how metrology, mechanical and environmental equipment are matched directly affects volume yield and delivery consistency.
From single 2D measurement toward multisensor fusion
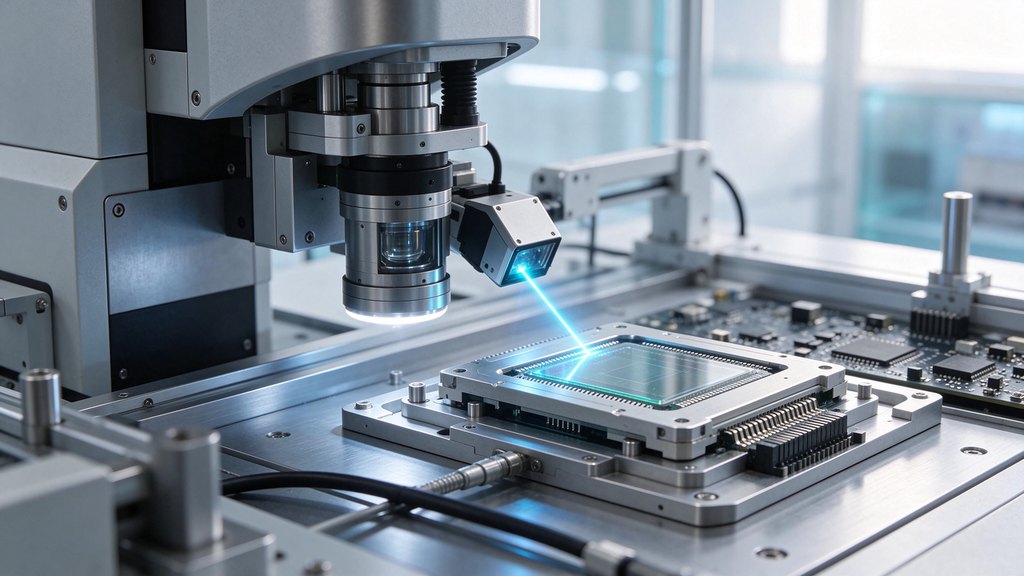
According to a Spectral Network industry review in July 2026, mid-to-high-end vision measurement equipment is moving from single 2D flat measurement toward an integrated architecture fusing optical imaging, line-laser scanning, white-light confocal and contact probes, so that 2D dimensions, 3D surface profile, surface defects and geometric tolerances can be checked in one workpiece clamping. This suits complex irregular thin-wall parts such as EV battery housings, foldable hinges and semiconductor package substrates; modular optical designs are spreading, with quick-swappable telecentric lenses and programmable ring coaxial lighting. The spread of 3D vision provides the base: as laser triangulation, white-light confocal, structured light and TOF sensors improve, flatness, warpage, step difference and profile measurement, along with robot guidance, can run in the same vision chain (Shanghai Securities News, April 2026).
Inline 100% inspection and offline precision inspection work in layers
Not all inspection belongs on the line; it is layered by value and cycle time. Leading Optics' inline warpage measurement equipment in September 2026 uses a dual scheme of "lab offline precision inspection plus line-side inline 100% inspection," building a warpage control loop from R&D to volume and addressing the limited capacity and missed defects of offline sampling. A November 2026 MRFR analysis of optical coordinate measuring machines notes that faster cameras and blue-light projection let high-value lines replace sampling with 100% inspection, while AI enters inspection planning: importing CAD and tolerances to auto-generate scan paths and classify deviations, shortening new-part introduction. A Stockstar report in August 2026, citing industry research, states that 3D AOI—with 3D profile metrology, height quantification and AI defect classification—has become standard quality equipment on advanced packaging lines.
Metrology, mechanical and environmental equipment each guard a reliability stage
A complete reliability setup is not only about dimensions. For size and profile, optical vision measurement equipment (video machines, CMM, projectors, microscopes) covers 2D contour, coordinate positioning, vision point picking and tolerance comparison. For force on materials and finished goods, mechanical and material testers run tension, compression, bending, insertion/extraction, life, vibration and abrasion tests, outputting force-displacement or stress-strain curves. For environmental fit, environmental reliability chambers simulate temperature-humidity, thermal shock, salt spray and aging to validate performance under sudden temperature change, humidity and corrosion. The three categories cover design validation, incoming sampling and volume monitoring respectively, and their data should flow back into process adjustment.
| Equipment | What it checks | Main stage |
|---|---|---|
| Vision/CMM metrology | Dimensions, contour, geometric tolerance and surface defects | R&D prototyping, incoming sampling and finished-size review |
| Mechanical/material testing | Tension, insertion/extraction, life, vibration, abrasion and force behavior | Material selection, structural strength validation and finished reliability confirmation |
| Environmental chamber | Temperature-humidity, thermal shock, salt spray and aging tolerance | Environmental validation and long-life assessment |
What this means for procurement and solution teams
When building inspection capability, first decide which parameters must be checked inline at 100% and which stay with offline metrology—avoid using high-end bench machines for line cycle time, and avoid treating precision metrology as a sampling-only formality. Selection should look at sensor combination, whether software connects to CAD and tolerances, traceability of data, and self-calibration and error compensation. For irregular thin-wall parts, first validate whether one clamping covers all required items; for long-supply categories, write mechanical and environmental test conditions into the acceptance criteria, which is more controllable than retesting afterward.
Comments
No comments yet. Be the first to comment.