
Equipment Lead Times and Delayed Capacity: Procurement Buffers
In mid-November, SMIC noted in an investor relations record that the global equipment supply chain remains tight, lead times are stretching, and some equipment originally expected to arrive this year has slipped to the next year; the company also said the industry has reached a consensus that AI-related manufacturing demand will stay tight through 2027, and capacity will be built to customer plans and demand. For hardware procurement, the takeaway is not just whether fabs expand, but that equipment lead times are pushing upstream capacity release later, and terminal scheduling and material stocking need to leave corresponding buffers.
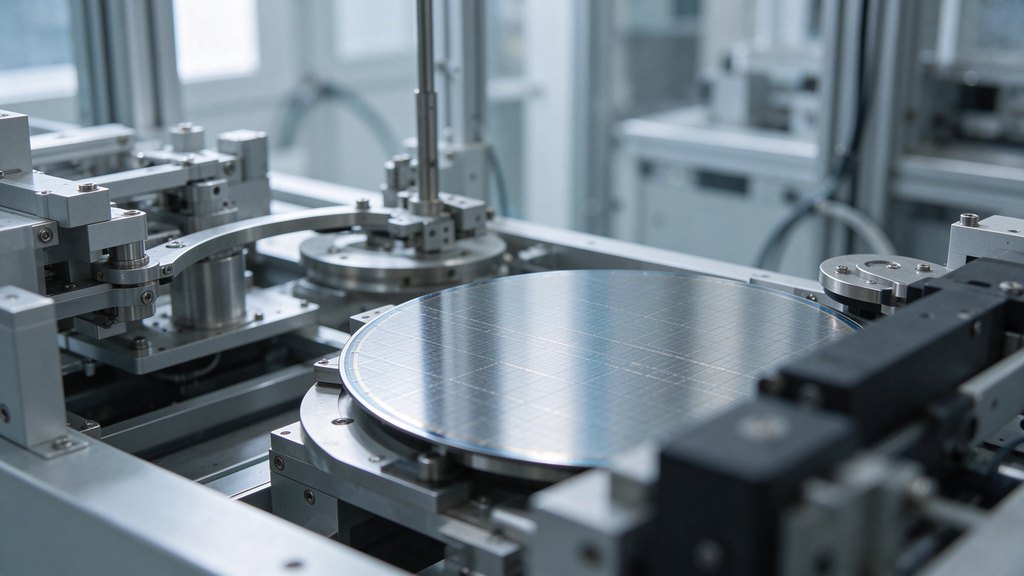
Longer equipment lead times push capacity release later
Wafer capacity does not land on order; equipment must arrive, be installed and tuned, then enter yield ramp. If delivery slips, actual output from new capacity moves later as well; in categories where demand stays tight, that slip directly slows the pace of available capacity. SMIC's record also said automotive chip orders have picked up notably since the second half of the year, with industrial and automotive coverage across BCD process, isolation devices and smart power switches; on dedicated memory, NOR Flash below 64M is roughly balanced while high-density products keep rising in price. Tightness is not uniform across categories, and the impact of delayed capacity transmits along product lines in layers.
Transmission along the chain: component supply and terminal scheduling affected in sequence
Equipment lead times first shape fab capacity plans, then transmit down through wafer, packaging and test, boards and systems. For upstream components, delayed capacity release means longer available supply cycles for some part numbers, and spot and contract prices and lead times are more likely to diverge; for terminal OEMs, scheduling should verify on-hand stock and lead times for key parts in advance, rather than assuming materials can be topped up against ideal capacity. It should be distinguished that this round of tightness comes more from equipment and capacity pace than from a sudden drop in demand, so how different terminals feel it depends on how scarce their parts are.
| Segment | How it is affected | Response focus |
|---|---|---|
| Wafer fabrication | New capacity releases with equipment arrival | Schedule to customer plans; track install and ramp progress |
| Upstream components | Scarce parts see longer available cycles | Split generic from dedicated parts; lock long-lead items early |
| Boards and systems | Key parts affect scheduling and delivery pace | Verify stock and alternates; roll forward stocking cycles |
| Procurement planning | Ideal-capacity assumptions need time margin | Separate committed orders from forecast stocking; hold inventory levels |
What this means for procurement and solution teams
Longer equipment lead times do not equal a blanket shortage; what really needs managing is pace and uncertainty. Procurement should split demand into committed delivery batches and forecast stocking: committed batches lock materials early for long-lead, capacity-tight parts, while the forecast side shortens replenishment cycles and controls inventory levels. Solution teams keep alternates and compatibility in the design, avoiding tying a single part number too tightly during capacity swings. Equipment arrival, yield ramp and spot prices by category should be tracked continuously before deciding whether stocking pace changes.
Comments
No comments yet. Be the first to comment.